
Australia’s warehouse market is projected to grow from US$3.78 billion in 2025 to US$8.68 billion by 2034, according to IMARC Group, with cold chain infrastructure and pharmaceutical distribution capacity named as a key segment driving that growth.
The supply chains behind healthcare and medical businesses will be crucial to capitalise on this projected growth. And compared to other sectors, they carry their own complexity.
Why medical supply chains get complicated
The Therapeutic Goods Administration, or TGA, is the regulator governing therapeutic goods in Australia, which ensures medicines, medical devices and other therapeutic goods supplied in Australia meet the right safety and quality standards. This means that following regulations is never a nice to have, it’s a must for any business.
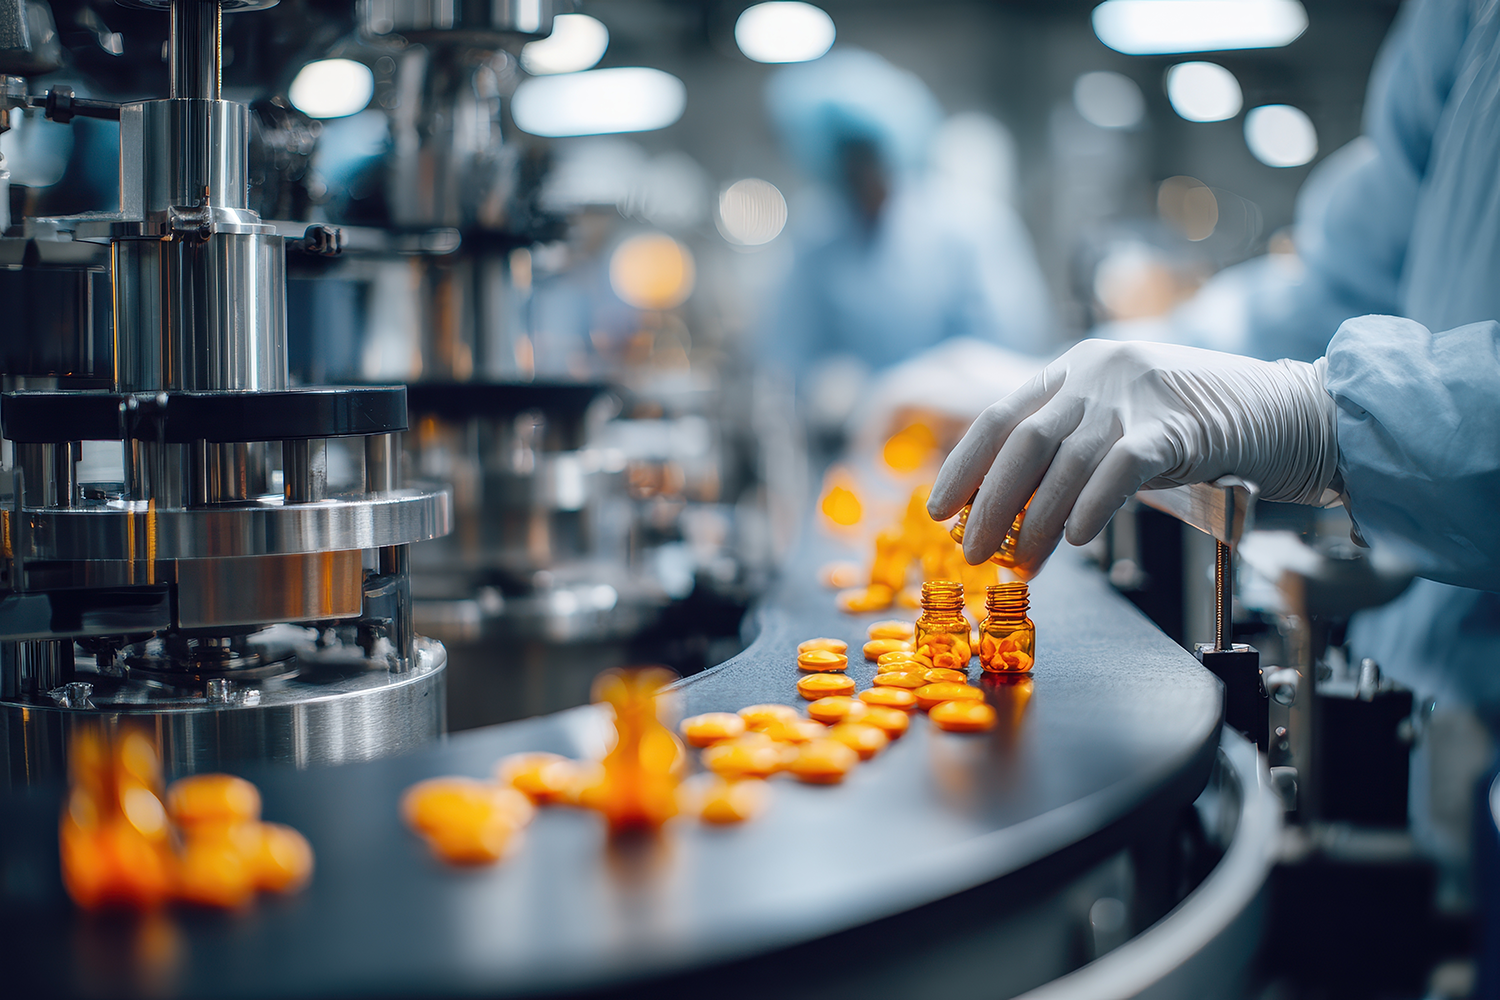
Unlike many industries, healthcare supply chains cannot treat compliance as an afterthought. Storage, security and handling requirements vary significantly across product categories, from secure vaults for controlled medicines to temperature-controlled environments and segregated storage for regulated products. These requirements influence everything from warehouse layout and material flow to scalability and automation decisions, making regulatory considerations a fundamental input into facility design rather than a final compliance check.
Robert Charles, Chief Operating Officer at ThreeSixty Supply Chain Group explains why medical supply chains require a different level of thinking.
“If regulatory requirements are not considered as part of the facility’s overall design and operational flow from the outset, they can create additional handling, operational bottlenecks and service delays. Over time, these inefficiencies can restrict a business’s ability to scale, adapt and respond to growth or changing customer and market demands,” Robert says. That inability to flex matters more in this sector than most, because the usual release valve, outsourcing overflow to a third party, sometimes isn’t available.
“With TGA licensing, you don’t always have the luxury of outsourcing overflow when your warehouse is full. For example, a business who needs to move product out of one facility might not be able to because the receiving site doesn’t hold the necessary licensing to accommodate it,” he says.
What designing around regulation actually looks like
Bringing compliance into a design process early doesn’t mean starting with the regulation. It means treating it as one of the inputs that gets factored in from the same starting point as throughput, growth and automation, rather than checked against once a layout is already drawn.
In practice, that tends to mean a few things happening before any layout decisions are made:
- Mapping the regulatory constraints specific to the product, not the category. A controlled substance, a temperature-sensitive biologic and a Class I medical device each carry different physical handling and storage obligations.
- Working closely with quality teams from the outset, not just mapping the regulation. In pharma, quality teams have significant input into how a facility operates. In many cases, businesses are not only designing to meet TGA requirements but also to satisfy global quality standards and internal compliance frameworks, which can be influenced by EU GDP and other international distribution practices.
- Modelling material flow against regulatory constraints, not just volume. Standard warehouse design starts with inbound and outbound profiles, growth projections and SKU behaviour. In this sector, segregation, security and traceability requirements need to be layered into that modelling from the outset, not tested against a layout after it’s been drawn.
- Testing more than one layout option against the same regulatory checklist. Where a constraint forces a trade-off, such as isolating a production area or building in dedicated quarantine space, comparing multiple options against the same compliance and efficiency criteria avoids defaulting to whichever layout is easiest to draw first.
- Considering automation as a core design input. Automation is a key consideration in healthcare and medical supply chains because it directly supports the need for faster fulfilment, greater accuracy and operational flexibility. The range of options is also broader than in many conventional warehouse environments, with A-frames, multi-shuttle systems and automated finishing solutions all being considered depending on product profile, order behaviour and service expectations. Given the value of the products being handled, and the importance of speed and flexibility in meeting market demand, the capital investment in automation can often be readily justified when it is designed into the facility from the outset.
- Designing for flexibility as demand and product needs change. Significant time and investment goes into getting a drug approved, and once it is, a business typically has a limited window of exclusivity before competition or substitution arrives. A facility needs to be designed to accommodate new product launches and shifting demand within that window, not just current volumes.
Designing with regulation, not around it
The businesses that get ahead in this space aren’t the ones bolting compliance onto an existing design. They’re the ones that bring regulatory and quality requirements into the conversation at the same time as throughput, automation and growth projections, rather than treating them as a separate workstream that only gets attention when something goes wrong.
As Robert points out, the cost of getting this wrong is major, showing up as increased handling, delays, falling service levels, and a business that
can’t grow or flex when it needs to. Designed well from the outset, a facility can do the opposite: hold its TGA-regulated complexity securely while still leaving room to grow, adapt to new product launches, and absorb whatever the next stage of demand looks like.